China Functional Masterbatch: Transforming Plastics with Advanced Color and Additive Solutions
2026-09-26
What if the vibrant colors in your plastic products could do more than just look good? In today’s competitive market, manufacturers need masterbatches that deliver both striking aesthetics and reliable performance — without hidden trade-offs. That’s where Xinwancai steps in. Our China functional masterbatch solutions are engineered to transform ordinary plastics into high-value, application-ready materials, combining advanced color dispersion with targeted additives for UV stability, flame retardancy, anti-static properties, and more. Whether you’re molding automotive parts, packaging, or consumer electronics, the right masterbatch can make all the difference. In this post, we’ll explore how Xinwancai’s innovative approach is reshaping what’s possible in plastic coloring and functionality — one pellet at a time.
Matching a Brand’s Exact Shade Across Multiple Resin Grades
Getting a brand color to look identical in a high-flow polypropylene and a glass-filled nylon is rarely as simple as using the same masterbatch letdown ratio. Base resin color, translucency, and additive packages shift the perceived shade even before processing heat history enters the picture. A blue that reads clean and bright in a natural PP can turn dull and slightly green in a grade with higher yellowness index or internal mold release.
The practical approach is to build a spectral fingerprint for each resin grade, not just for the target color. Measure the raw substrate with a spectrophotometer, then adjust pigment loading and sometimes swap a pigment entirely to compensate for the base tint. Small changes in titanium dioxide level or the addition of an optical brightener can pull a shade back into tolerance without altering the visual texture of the part.
When multiple grades must share one brand identity, agree on a color tolerance box in CIELAB space and verify under at least two illuminants, typically D65 and a fluorescent store light. Batch records should note the specific resin grade, melt temperature, and even regrind percentage, because all of these can nudge the final appearance away from the approved standard.
Additive Systems That Take the Heat, Light, and Static
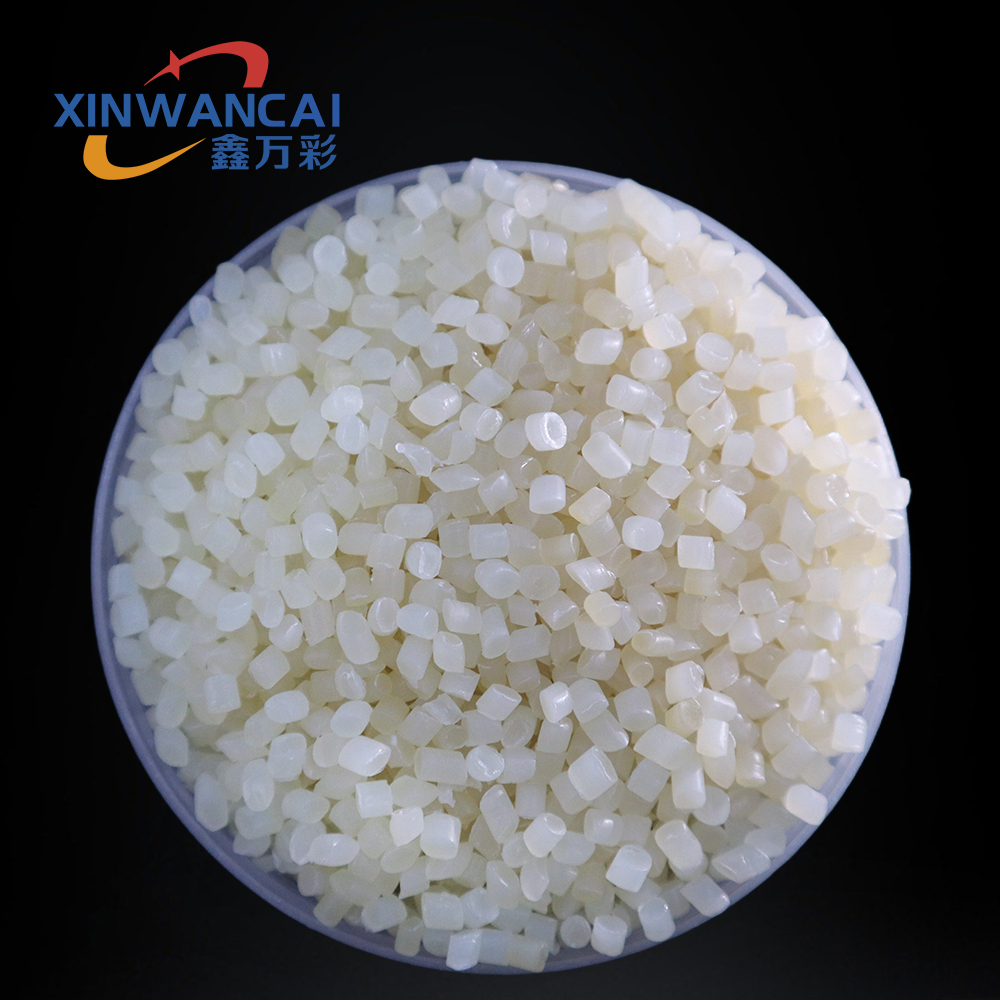
In real-world use, plastics and coatings rarely fail from a single stressor. Heat fades colors and weakens polymer chains, UV light triggers chain scission and yellowing, and static buildup attracts dust while posing risks in electronics handling. A well-designed additive package addresses all three without forcing compromises in clarity, mechanical strength, or processing window.
Heat stabilizers, often based on hindered phenols, phosphites, or lactones, interrupt thermal oxidation cycles before they degrade the base resin. Light stabilizers—typically hindered amine light stabilizers (HALS) and UV absorbers such as benzotriazoles—quench excited states and scavenge free radicals generated by sunlight or artificial lighting. Static control usually comes from migratory antistatic agents or permanent conductive additives like carbon nanotubes or ionomers, depending on whether the need is temporary surface conductivity or long-term dissipation.
The trick is balancing these chemistries so they don't cancel each other out. Some antistats can plasticize and reduce heat deflection temperature; certain UV absorbers may interact with metal-based heat stabilizers. Formulators often turn to synergistic blends—for example, a high-molecular-weight HALS paired with a low-volatility phosphite and a non-blooming antistat—to maintain performance across demanding thermal, optical, and electrical conditions.
Thin-Wall Molding Without the Warp: The Role of Masterbatch
Thin-wall molding pushes every material to its limit. When part thickness drops below one millimeter, flow resistance spikes, cooling becomes uneven, and internal stress stacks up fast. That stress is what usually shows up later as warpage, whether it's a slight bow across a flat panel or a twist in a tall, slender housing. The resin alone often cannot hold the part's shape once it leaves the tool. This is where a well-chosen masterbatch does more than add color; it changes how the melt fills, packs, and shrinks.
Traditional black masterbatches built around coarse carbon black can act like tiny speed bumps inside the melt stream. They increase viscosity just enough to make thin sections fill unevenly, amplifying orientation stress along the flow path. In contrast, a high-flow masterbatch with a tailored carrier resin and fine particle dispersion allows the polymer to slip through narrow gates and ribs more uniformly. The result is a more balanced shrinkage profile, meaning the part cools with less locked-in tension. Warp is not eliminated by luck; it is reduced by giving the melt fewer reasons to pull against itself.
Beyond rheology, masterbatch selection also influences how the part releases from the mold and how it behaves during post-molding handling. A masterbatch with a low coefficient of friction can ease ejection without added mold release sprays, preventing ejection-induced bending on delicate thin walls. Meanwhile, the right nucleating agent inside the masterbatch can promote finer, more uniform crystallinity in semi-crystalline resins, further tightening the gap between intended and actual geometry. In thin-wall work, these details stop being minor. They become the difference between a flat, stable part and one that arrives at the assembly line already fighting its own shape.
Recycled and Bio-Based Carriers That Skip the Gray Cast
Plenty of recycled and bio-based plastics have a reputation for looking a bit muddy. The impurities in post-consumer waste or the natural tone of plant-derived polymers often create that unwanted gray or yellowish haze. But a new wave of carrier materials turns that assumption on its head. Through tighter sorting, purification steps, and the use of clarified bio-resins, these carriers come out with a clean, bright appearance that rivals virgin plastics. They drop the dullness without dropping the sustainability story.
The trick lies in how the feedstock is handled. Instead of blending mixed-color bales, manufacturers select specific streams like clear PET bottles or white HDPE containers. For bio-based options, fermentation-derived building blocks can be polymerized into resins with fewer chromophores—those molecular structures that absorb light and create a gray tint. Some producers also add optical brighteners or carefully balanced colorants to mask any residual haze. The result is a carrier that looks crisp on the shelf, not like it came from a recycling bin.
This matters more than people expect. A gray cast can make a product feel cheap or dirty, even if it's environmentally sound. By eliminating that visual clue, brands get to communicate their green credentials without compromising on shelf appeal. Retailers and consumers notice the difference—and they reward it.
Low-Odor, Low-VOC Formulations for Interiors and Food Contact
The push toward low-odor, low-VOC systems in interior coatings and food-contact materials has forced a move away from traditional solvent-borne chemistries. But lowering VOC content alone rarely solves the odor problem, because many exempt solvents and some reactive diluents can still carry sharp or lingering smells. A more reliable route combines high-solids or waterborne binders with carefully selected coalescents and wetting agents that have low vapor pressure and minimal residual monomers. For interiors, this often means benchmark testing against methods like ISO 16000 or California CDPH emissions; for food contact, the challenge is balancing emission performance with migration limits under FDA or EU regulations.
One overlooked area is the interaction between resin neutralization and odor. Amine-neutralized waterborne systems, for example, can generate noticeable ammonia-like or fishy notes as films dry, especially in low-air-exchange rooms. Switching to non-amine stabilizers or designing polymer particles that require less hydrophilic modification can reduce both odor and the amount of high-boiling co-solvent needed. Similarly, replacing traditional photoinitiators or cobalt driers with odor-free alternatives matters just as much as the main solvent choice. These adjustments often improve shelf stability and lower total formulation cost because fewer masking agents are needed.
In food-contact applications, low odor is not simply a comfort issue; it is directly tied to sensory taint. A coating or adhesive that passes migration testing may still fail organoleptic panels if trace residuals alter taste or smell of packaged food. Successful formulations typically minimize low-molecular-weight species, use polymeric surfactants rather than small-molecule ones, and include a post-cure or vacuum stripping step to pull out volatile by-products. Field experience shows that robust low-odor performance comes from consistency in raw material sourcing and a willingness to reformulate around actual end-use conditions, not just regulatory minimums.
Shortening the Custom Color Approval Cycle From Weeks to Days
Traditional color approval processes often drag on because physical samples shuttle between designers, suppliers, and decision-makers. Each round of courier delays, lab dip adjustments, and email chains adds days that nobody can afford. By shifting to digital color standards and centralized review platforms, teams can collapse those waiting periods into a single afternoon of focused feedback.
The real bottleneck is rarely the dyeing itself—it's the back-and-forth over vague comments like "a touch warmer" or "slightly less red." Replacing those subjective calls with spectral data and calibrated on-screen evaluations lets everyone see the same color at the same time. When the approval workflow is tied to real-time measurements instead of physical swatches, iteration cycles drop from weeks to hours.
Some brands are already cutting approval time by 80% simply by letting remote stakeholders annotate digital color proofs instead of waiting for overnight packages. The key is making the process feel less like a handoff and more like a shared workspace—where approvals, rejections, and tweaks happen in one continuous thread. Once teams experience that speed, going back to the old courier-based cycle feels unthinkable.
FAQ
Ordinary color masterbatch mainly handles pigmentation. A functional version also carries additives like UV stabilizers, flame retardants, antistatic agents, or antimicrobials. The tricky part is keeping those additives from interfering with color development, so formulation work tends to be far more involved.
Many Chinese producers now run twin-screw extruders with precise feeding and inline spectrophotometers for color control. Combined with lower overhead and a deep raw material supply chain, they can often deliver custom batches in two to three weeks that would take much longer elsewhere.
It gets dosed into the resin at a small percentage, usually between 1% and 5%. The pellet melts and disperses, altering surface resistivity, UV resistance, scratch behavior, or flame performance. The base polymer remains the same, so processors avoid re-qualifying an entirely new material.
Thin-wall food packaging often needs both bright color and oxygen or moisture barrier help. Agricultural films need UV protection plus anti-drip or infrared retention. Automotive trims need exact color and resistance to heat and light. Each application pushes formulation in a different direction.
Vague answers about carrier resin, no dispersion data, inconsistent pellet size, or refusal to share a sample with full technical data sheet are red flags. Also beware suppliers who promise very high additive loading without explaining how they prevent agglomeration.
It can, but interaction effects matter. Some antioxidants can shift color, some flame retardants can cause plate-out, and too many additives can reduce tensile strength. A good supplier will run thermal stability and mechanical tests on the final compound, not just on individual ingredients.
If the carrier doesn't match the base polymer, you may see poor dispersion, surface defects, or even delamination in multi-layer films. For polypropylene parts, a PP-based carrier is standard; for polycarbonate, a PC-compatible carrier avoids haze and impact loss.
Conclusion
China's functional masterbatch sector has moved far beyond simple color dosing. A single brand shade now needs to hold across PP, ABS, PC, and even recycled streams without visible drift. That means pigment dispersion, carrier resin compatibility, and thermal history all have to be engineered together, not adjusted after the fact. The same batch of masterbatch often carries co-additives that protect against UV fading, heat aging, and static buildup, which is why processors can skip separate dosing steps. For thin-wall packaging and electronic housings, the right nucleation package and internal lubricants in a masterbatch can reduce warpage enough to avoid costly tooling changes or post-mold straightening.
Recycled and bio-based carriers are no longer a compromise on brightness, as advanced stabilizer blends prevent the dull gray or yellow cast that used to plague PCR-rich compounds. Low-odor, low-VOC grades are now standard for automotive interiors and food-contact applications, where emission limits are tight and odor panels are part of acceptance. Meanwhile, custom color matching has shifted from mailing physical chips back and forth to cloud-based spectral data and small-batch lab extrusion, cutting approval loops from weeks to a few days. That speed matters more than most realize, because a delayed shade sign-off can stall an entire product launch. Chinese masterbatch suppliers are increasingly expected to act as material performance partners, not just pigment vendors.
Contact Us
Contact Person: JACK
Email: [email protected]
Tel/WhatsApp: 86 18650130917
Website: https://www.xinwancai.com/