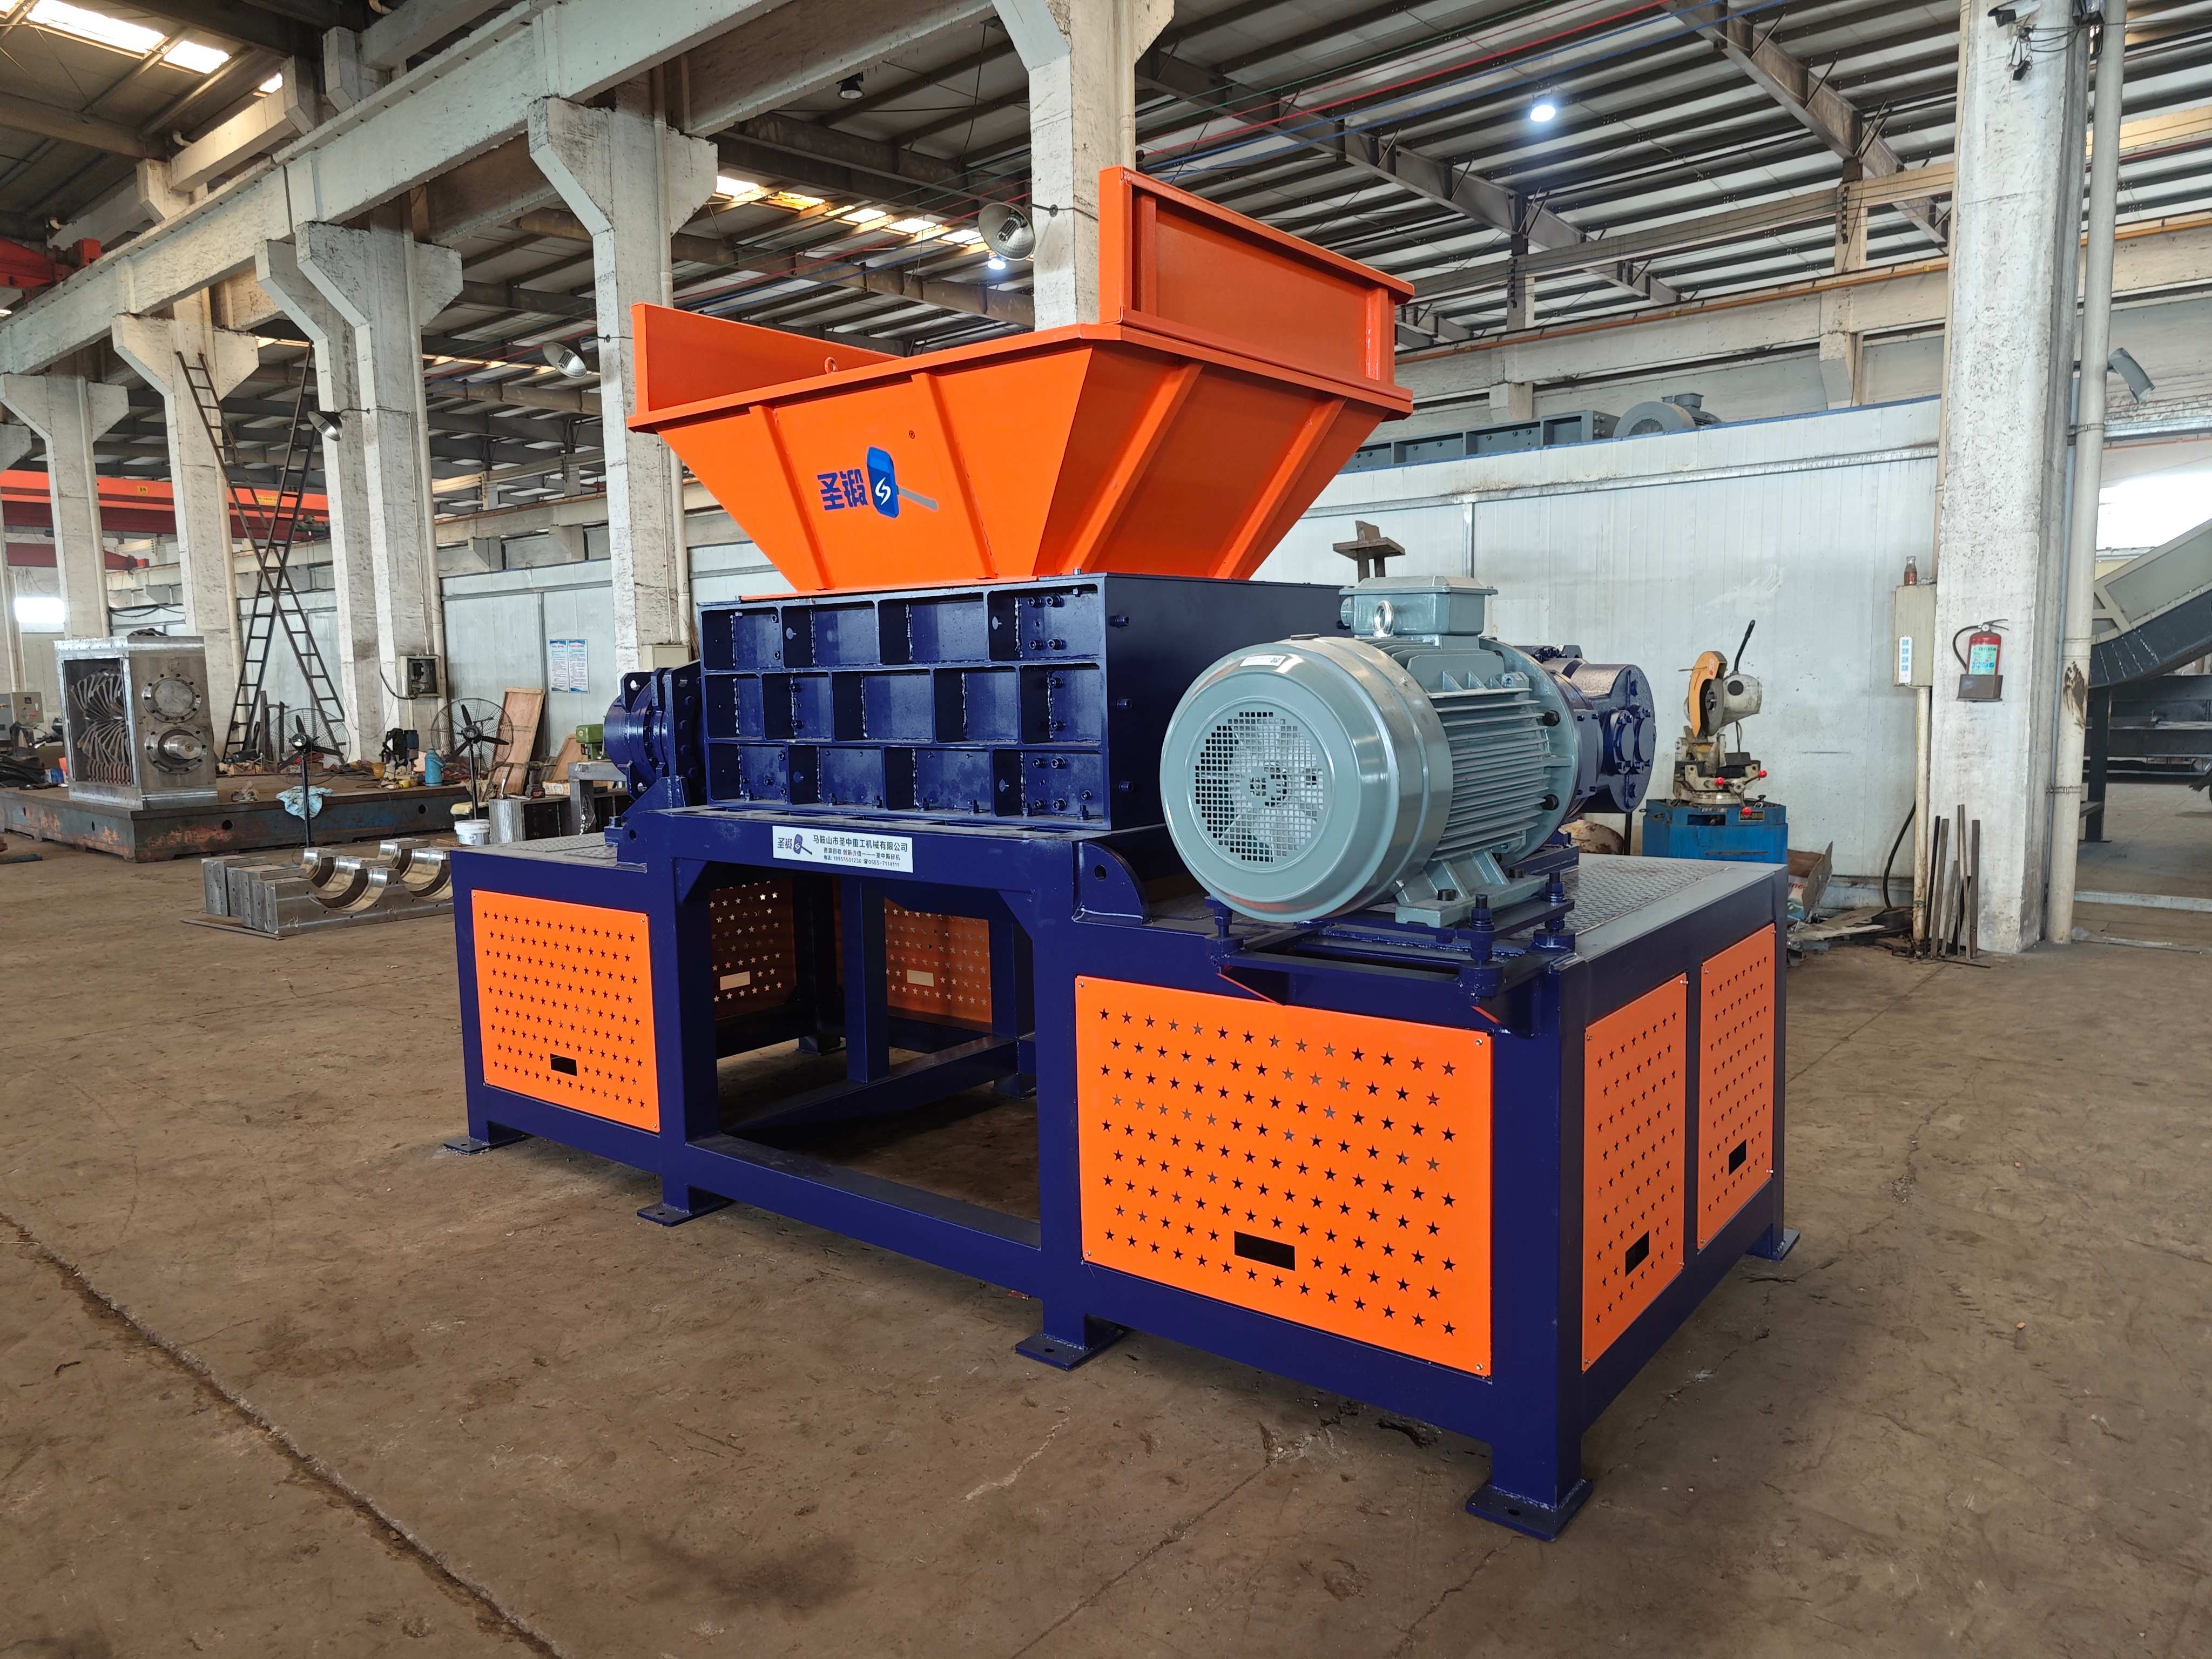
Four Shaft Shredder by a Powerful Manufacturer for Heavy-Duty Performance
2026-11-01
Some materials don’t just resist shredding—they punish the machine. If your current line struggles with bulky, high-torque waste, a four shaft shredder built by Shengzhong Shredder changes the equation. Heavy-duty performance here isn’t a spec-sheet claim; it shows up in tighter particle control, fewer jams, and longer runs between maintenance. In the sections ahead, we’ll break down what makes this design different.
Four Shafts, One Goal: Shredding Without Compromise
Most multi-shaft shredders promise power, but the real difference shows up when four independent shafts meet unpredictable feed material. Instead of relying on a single pair of rotors to do all the work, a four-shaft design distributes the load across two overlapping cutting zones. That means less jamming, lower peak torque on any one shaft, and cleaner shearing action through mixed waste streams.
The four shafts are not just stacked for show. Each shaft pair runs at a slightly different speed, creating a tearing and pre-cutting stage before the final sizing pass. This staged reduction lets the machine take in bulky, awkward items without forcing the operator to pre-sort or pre-cut. The result is a steady output size, even when the infeed swings from plastics to thin-gauge metals to wood offcuts.
Shredding without compromise means the machine shouldn't ask you to choose between throughput, particle consistency, and uptime. Four shafts let you keep all three. The lower individual shaft load reduces wear on bearings and cutters, and the overlapping cutting paths make blade changes more predictable. For operations that can't afford to baby a shredder, that's the whole point.
Inside the Engineering That Keeps Blades Aligned Under Load
Long composite blades don't hold their chord line by stiffness alone. At the root, a preloaded stud circle with ovalized bushing seats keeps the flange from slipping under flapwise bending, while a controlled-friction shim lets the pitch bearing rotate without breaking the clamped boundary. The trick is to set that boundary stiff enough for bending loads but soft enough for thermal growth, so a gust doesn't turn into a permanent half-degree of pitch error.
Halfway outboard, the spar cap gets a slight off-axis fiber bias, usually two to three degrees, to fight shear lag that would otherwise twist the neutral axis under peak loads. Trailing-edge reinforcement doubles as a shear web anchor, stopping the aerodynamic center from drifting aft when the blade flexes. Strain gauges near the max chord station then feed a real-time correction to the pitch actuator, nudging the blade by fractions of a degree before the yaw error becomes visible at the generator.
A Manufacturer’s Track Record in Heavy Industry
A manufacturer’s track record in heavy industry is not built on brochures or launch events; it lives in the cold starts, overloaded cycles, and unplanned shutdowns where equipment either holds or fails.
Look beyond the total number of units shipped. Pay attention to how many early models are still running a decade later, how often the same customers return for expansions, and whether the field service reports show repeat fixes or genuine root-cause resolutions. In mining, steel, cement, and port logistics, the most credible manufacturers can point to specific machines that outlived their original depreciation schedules and to maintenance teams that stopped treating certain breakdowns as routine.
The Case for Redundant Cutting Stages in Bulk Reduction
Relying on one aggressive cutting stage for bulk reduction often looks cleaner on paper, but real feed material rarely behaves. Hard inclusions, moisture swings, and unexpected tramp objects can stall a single-stage setup without warning. Redundant stages act as a buffer: when the first unit bogs down or trips, the downstream cutter keeps processing whatever passes through, buying time for operators to respond instead of shutting the whole line.
There is also a less obvious energy logic. A single stage forced to span from large lumps to fine output wastes power through overgrinding and heat. Splitting the work across two or three stages lets each machine run in its efficient range—coarse cutters handle high torque at low speed, while finer stages run faster on already reduced material. The result is lower specific energy per ton and longer wear life on every cutting element.
Then comes the matter of final particle control. The last stage in a redundant setup receives a much more uniform feed because the rough work has already been absorbed upstream. That steadier input makes it far easier to hold a tight size distribution, which downstream mixing, conveying, or chemical processes often demand. Without those earlier cutters doing the heavy lifting, the final stage would constantly chase a moving target.
What Happens When Unshreddable Debris Meets This Machine
When unshreddable debris—stuff like thick steel cables, solid chunks of concrete, or tangled masses of industrial rubber—hits the feed chute, most machines would jam in seconds. But this one doesn't flinch. Instead of relying on brute-force cutting blades, it uses a combination of high-torque rollers and pressure zones that slowly crush and tear materials apart at their structural weak points. The result is a steady, almost meditative grind that reduces the impossible into uniform, manageable pieces.
The key is in the machine's adaptive resistance. It senses material density and automatically shifts its internal geometry, widening gaps for bulky items and tightening them for fibrous tangles. You can feed it a mix of scrap metal, demolition waste, and even old tires, and it will sort through the chaos without clogging. Operators often describe the sound as a low, rhythmic crunch—nothing like the violent screaming of a conventional shredder.
What really surprises first-time observers is the absence of sparks or flying shrapnel. The debris is pulled inward, fractured by compression, then ejected as consistent fragments that fall neatly onto a conveyor. It's the kind of machine that makes you wonder why anyone still builds shredders with spinning blades at all.
From Mixed Waste to Consistent Output: A Closer Look
The journey from a jumbled stream of household and commercial refuse to a dependable feedstock or fuel is rarely a straight line. Sorting facilities face constant variation: one hour the line is heavy with soggy cardboard, the next it's a surge of thin plastic film and broken glass. Achieving steady output means treating the incoming material not as waste but as a variable raw material whose moisture, density, and particle size all shift by the minute. Operators learn to read these shifts early, adjusting air knives, screen angles, and magnet settings before the line drifts out of spec.
The closer look reveals that consistency is rarely solved by a single machine. It comes from layering complementary separation stages: a drum screen that spreads material evenly, an eddy current separator pulling non-ferrous metals, optical sorters tuned to specific polymer signatures, and manual pickers catching what sensors miss. Each stage removes a slice of the variability, and the cumulative effect is what turns a chaotic input into a baled output that a downstream mill can actually trust.
Even with good equipment, the human factor remains decisive. Same plant, same feedstock, different shift leads can produce different bale quality. That's why tighter operations now track reject rates by hour, not by day, and recalibrate optical sorters at shift changes. Small routines—cleaning sensor lenses, checking air pressure, re-zeroing conveyor speed—stack up into the difference between a load that meets spec and one that gets rejected at the gate.
FAQ
It handles a broad range of tough inputs, including industrial scrap, tires, electronic waste, metal turnings, and dense plastics. The extra cutting stages break material down evenly, so even stringy or bulky items pass through without wrapping around the shafts.
The lower pair of shafts acts as a secondary sizing stage, recirculating oversized pieces until they meet the screen's opening. This avoids the random chunks you sometimes get from two shaft machines and gives you a consistent particle size for downstream processing.
You're working with a company that runs its own stress testing and provides on-site commissioning, spare parts warehousing, and direct access to engineers. They don't just sell the machine; they stay involved through wear part replacement and performance audits.
Yes, the frame and gearbox are built for continuous duty, with oversized bearings and a cooling circuit on the hydraulic drive. Many sites run it around the clock and only stop for scheduled knife rotation or cleaning.
Daily checks include inspecting the knives for dull edges, clearing any debris from the screen area, and verifying the hydraulic oil temperature. Weekly you'll want to torque the knife bolts and check ram guides, then rotate or replace cutters based on wear patterns.
You can choose hook, square, or combination teeth with varying thickness and hardness. The screen basket is also swappable, so the same machine can produce coarse chunks for incineration or fine pieces for material recovery.
The shredder includes an auto reversing function that detects overloads and clears blockages without manual intervention. E-stop cords run along the feed hopper, and the access doors are interlocked so the rotors can't spin during maintenance.
It can be fitted with discharge conveyors, magnetic separators, and dust hoods. The control cabinet supports common industrial protocols, so your existing PLC can monitor load, temperature, and throughput in real time.
Conclusion
Heavy-duty shredding leaves no room for compromise, and the four-shaft configuration from this manufacturer is built around that reality. Each cutting stage is arranged so that material passes through redundant, counter-rotating shafts before discharge, which keeps the output fraction consistent even when feed streams swing from bundled plastics to metal-clad waste. The blade alignment under load is not left to chance. Machined bearing housings, oversized shafts, and a rigid frame hold tolerances when torque peaks, so the cutting gaps stay tight without constant adjustment. That kind of engineering puts the machine in a different class from lighter single- or twin-shaft units, especially for facilities that cannot afford surprise downtime.
When unshreddable debris such as a solid steel bar or a loose excavator tooth enters the chamber, the drive system responds by reversing or stopping the affected shaft before damage spreads—an approach that protects not only the blades but also the downstream conveyor and separation equipment. The manufacturer's record in heavy industry supports that claim. Cement plants, scrap yards, and municipal processing lines run these units for years with scheduled blade rotations rather than emergency rebuilds. Mixed waste, whether from construction debris or bulky commercial loads, ends up reduced to a uniform particle size that screens and magnets can actually process. That consistency, combined with the brute force of four independently driven shafts, is what makes this shredder a reliable anchor for high-volume reduction.
Contact Us
Contact Person: Leon
Email: [email protected]
Tel/WhatsApp: 8615385558866
Website: https://www.shred-waste.com