HC-22 Nickel Based Alloy Extruded Seamless Pipe Supplier: Your Complete Sourcing Guide
2026-11-01
Sourcing HC-22 nickel alloy extruded seamless pipe isn’t just about finding a supplier—it’s about avoiding costly mismatches in corrosion resistance, pressure ratings, and dimensional tolerances. This guide cuts through the usual spec-sheet noise and walks you through what actually matters when qualifying an HC-22 pipe source. Along the way, you’ll see why JILAIDA has become the go-to name for buyers who need consistent extrusion quality and traceability, not just a one-time shipment. Whether you're replacing failed piping or specifying a new high-temperature loop, the next few sections will help you source with confidence.
Where HC-22 Actually Earns Its Premium Over Standard Nickel Alloys
The premium for HC-22 over standard nickel alloys like 625 or C-276 often gets justified the moment a process stream mixes oxidizing and reducing acids. Standard grades tend to be specialists—they handle either chloride-rich oxidizing conditions or hot reducing acids, but rarely both without pitting or crevice attack. HC-22's balanced chromium, molybdenum, and tungsten content lets it sit comfortably in wet, aggressive environments where the pH swings or chlorides sneak in, which is exactly where cheaper alternatives start to fail.
Welding is another place where the price difference disappears in practice. Many nickel alloys require careful heat control and post-weld heat treatment to avoid sensitization and intergranular corrosion. HC-22, by contrast, holds up well in as-welded condition on most thicknesses. That means fewer shop hours, less risk of rework, and no extra furnace cycles—savings that make the upfront material cost far less intimidating.
Then there is the matter of long-term performance in critical equipment like reactors, scrubbers, and piping exposed to mixed acid streams or seawater-cooled process lines. With standard alloys, you may get a lower purchase price but inherit a maintenance schedule that eats up the difference within a couple of turnaround cycles. HC-22 tends to stay cleaner longer, resist localized attack that forces unplanned shutdowns, and ultimately deliver a lower total cost of ownership across a decade or more of service.
Why Extruded Seamless Construction Matters for HC-22 Pressure Systems
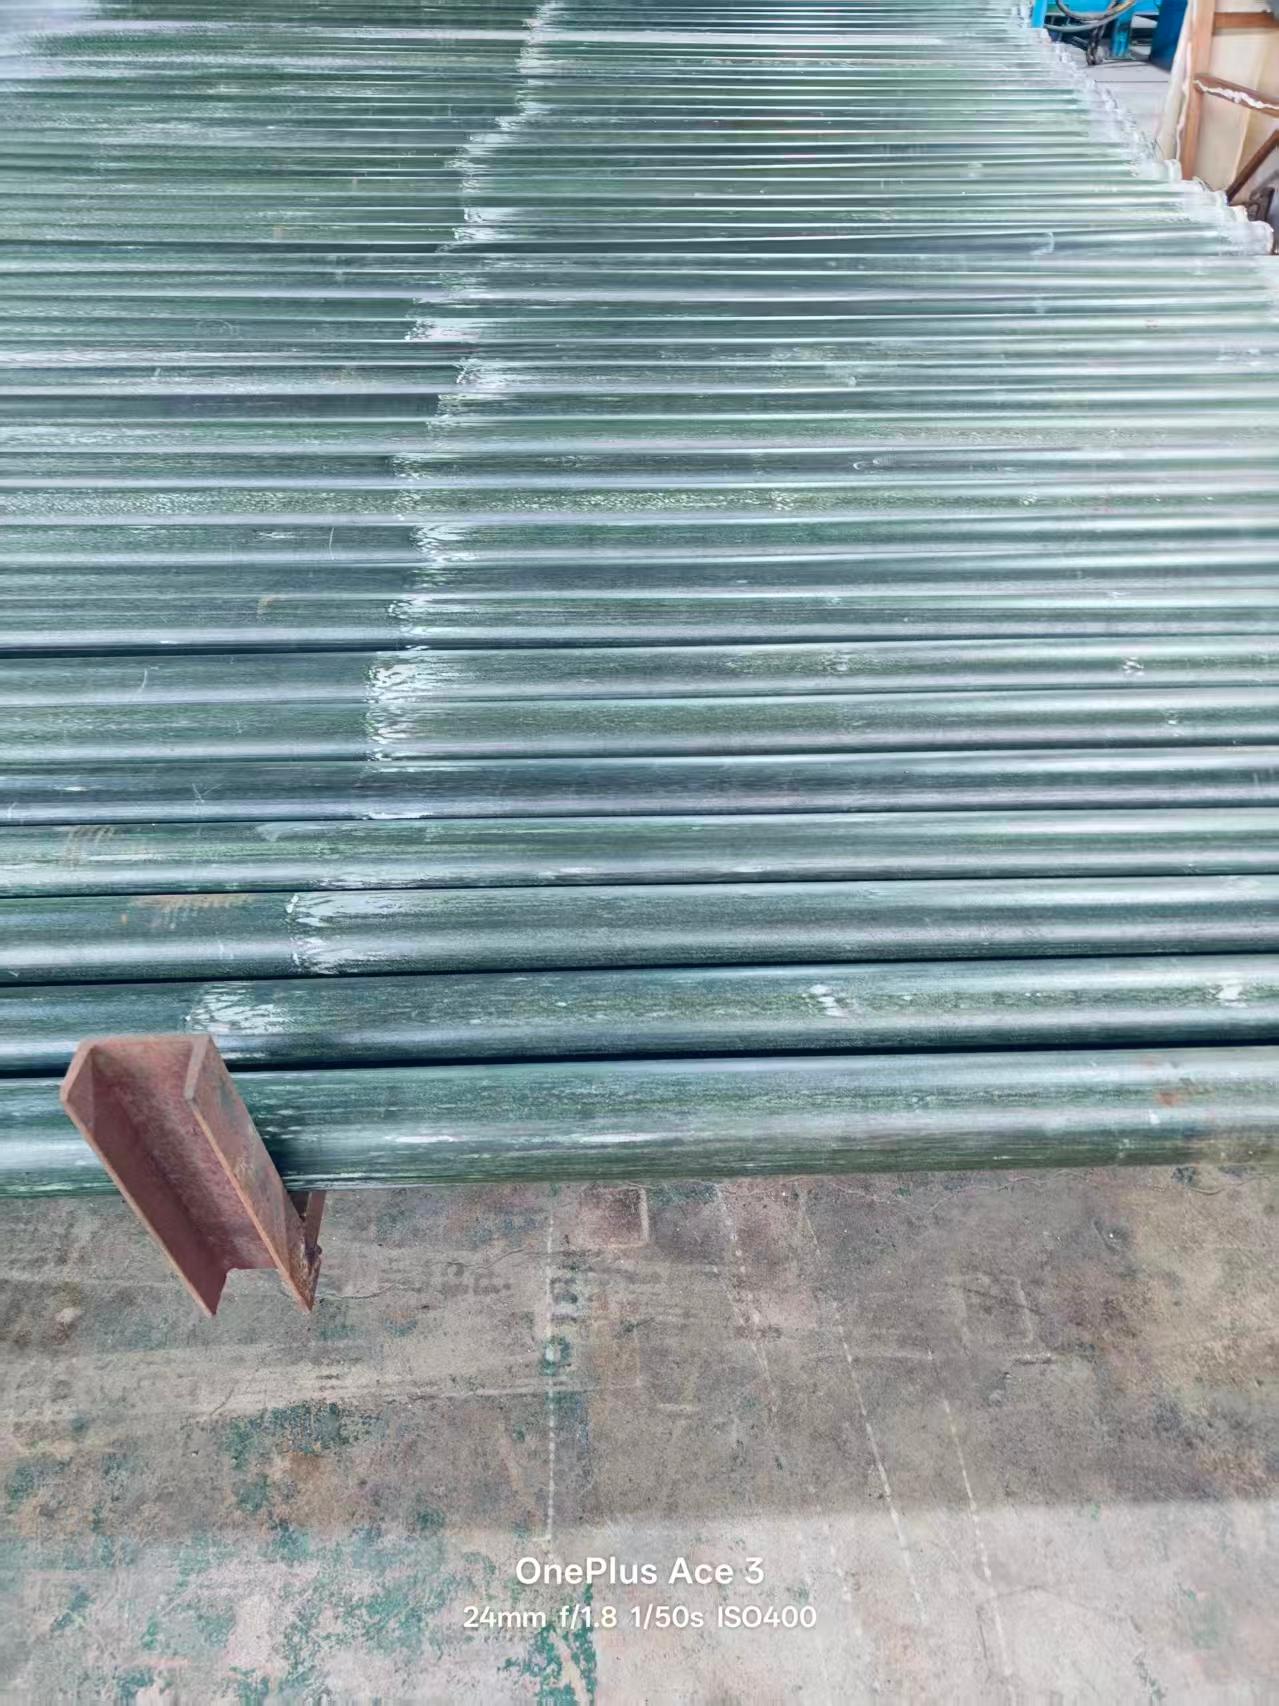
In HC-22 pressure systems, the absence of a weld seam is not a minor detail—it is the difference between a component that withstands cyclic stress and one that eventually cracks. Extruded seamless construction eliminates the heat-affected zones and residual stresses that welded pipe typically carries. For a nickel-chromium-molybdenum alloy like HC-22, this means the corrosion resistance remains consistent across the entire wall thickness instead of weakening near a seam. When the system experiences repeated pressure fluctuations, that uniformity translates directly into longer service intervals and fewer unplanned shutdowns.
Beyond fatigue resistance, the extrusion process refines the grain structure in a way that roll-and-weld methods cannot match. The metal flows in a single continuous operation, producing a dense, homogeneous wall without the microscopic porosity or inclusions that can hide along a weld line. In aggressive chemical environments—where chlorides, acids, or hot process fluids are common—these small imperfections often become initiation points for pitting or stress corrosion cracking. By choosing extruded seamless HC-22 components, engineers remove those initiation points before the system is ever pressurized.
The Supplier Questions Most Buyers Forget to Ask Until It's Too Late
Most sourcing conversations start with unit price, minimum order quantities, and delivery windows. Those numbers matter, but they rarely reveal how a supplier behaves when something breaks. Buyers often forget to ask what happens when the supplier's own material source goes down, or what contingency plans exist for a key machine that needs a month of downtime.
A handful of questions get skipped because they feel awkward or overly detailed. For example: 'Who actually owns the tooling if our contract ends?' 'Can we review your internal rejection rates from the last two quarters?' 'How do you absorb a sudden 30 percent jump in demand without cutting corners on tolerances?' These aren't hostile questions; they expose whether a supplier has real operational discipline.
By the time a buyer realizes the answers matter, there's usually a shipment stuck at the border, a batch that doesn't meet spec, or a tooling dispute with no clear paperwork. Asking early costs nothing. Waiting until production is live turns a simple question into an expensive lesson.
How to Spot Inconsistencies in HC-22 Mill Test Reports
Begin by comparing the heat number and product description across every page of the report. A single digit transposed in the heat code or a mismatched grade designation often signals a deeper documentation error. Check the revision date against the purchase order and the actual production date—if the report was revised after the material shipped, ask why. Look for gaps in the sequence of mechanical test results; a missing tensile or yield entry can mean the data was pulled from a different coil or plate. Pay attention to the signature block as well. Signatures that appear copied, blurred, or use a generic font rather than a handwritten or verified digital mark deserve closer scrutiny.
Next, cross-check the chemical composition against the specified range for HC-22. Values that sit exactly on the upper or lower limit for multiple elements are statistically unusual and may indicate rounded or fabricated numbers. Trace the trace elements—boron, titanium, aluminum—because small deviations there affect weldability and corrosion resistance more than the headline alloying elements. If the report lists results for tests that were not required by the governing standard, question why they are included. Extra data can be a distraction from missing critical tests, such as intergranular corrosion or impact toughness at low temperature.
Finally, verify the lab accreditation and the identity of the testing facility. A legitimate report will reference an ISO/IEC 17025 scope that includes the specific test methods used. If the lab name is incomplete, misspelled, or the accreditation number does not match the country of origin, treat the document as suspect. Compare the report's format with other certificates from the same mill—real mills maintain consistent templates, paper watermarks, and digital seal placement. Inconsistencies in line spacing, logo resolution, or the order of sections often reveal a cut-and-paste job. When any single data point cannot be traced back to a raw test record, request the original lab notebook or an accredited third-party re-test before accepting the material.
What Realistic Lead Times Look Like for Custom HC-22 Pipe Orders
Custom HC-22 pipe orders rarely follow the same timeline as stock material. Depending on outside diameter, wall thickness, and whether the pipe requires hot finishing or cold pilgering, you’re generally looking at twelve to twenty weeks from drawing approval to shipment. Smaller diameters in common schedules can sometimes be squeezed into eight to ten weeks when a mill has a matching billet or hollow already in process, but anything with non-standard chemistry tweaks or tight ovality tolerances adds another three to five weeks on top.
A lot of the delay comes down to raw material sourcing. HC-22 requires nickel, chromium, and molybdenum in specific ratios, and mills don’t keep every ingot size on the shelf. If your order calls for an uncommon OD-to-wall ratio, the foundry may need to cast a dedicated ingot or convert a larger billet, which pushes the front end of the schedule. Surface conditioning, ultrasonic testing, and final passivation also eat up time, especially when third-party inspection is involved. Planning for sixteen weeks as a baseline is safer than banking on a best-case quote.
Shorter lead times are possible on paper, but they usually come with compromises: limited size ranges, relaxed testing, or an expedite fee that doesn’t always guarantee faster delivery. The most reliable way to keep a custom HC-22 pipe order moving is to lock in the mill’s production window early and avoid last-minute spec changes. Once the pipe enters the cold working stage, any revision to length, end finish, or marking requirements can set the schedule back by a week or more.
The Hidden Cost Drivers Behind HC-22 Pipe Quotes
Most buyers fixate on the base price per meter, but HC-22 pipe quotes routinely carry markups that trace back to nickel and molybdenum index swings. Mills don't absorb these moves; they pass through monthly alloy surcharges that can shift a seemingly firm number by double digits before the PO is cut.
Another quiet leak is nondestructive testing. If your spec calls for 100% ultrasonic or eddy current inspection on every length, expect the quote to climb well beyond the raw tube cost. Smaller diameters and heavier walls amplify this because fewer producers keep that tooling online for short runs, and setup charges get distributed across a smaller lot.
Finally, watch for documentation and packaging clauses. EN 10204 3.2 certification, positive material identification on each heat, export crating, and inland freight to a non-port city rarely appear as line items. They sit in the margin, which is why two quotes for the same schedule can diverge by 20% while the stated alloy surcharge looks identical.
FAQ
HC-22 is a nickel-chromium-molybdenum alloy with tungsten, giving it far superior resistance to pitting, crevice corrosion, and stress corrosion cracking in aggressive environments compared to common stainless steels. The extruded seamless process eliminates weld seams, which removes weak points and ensures uniform mechanical properties along the entire length.
You will find it in chemical processing, pollution control, pulp and paper, waste treatment, and marine engineering. Anywhere that handles hot, contaminated acids or chloride-rich streams tends to require HC-22's reliability. It also shows up in pharmaceutical and food processing equipment where contamination resistance matters.
Ask for a material test report or mill certificate that shows chemical composition and mechanical properties per ASTM B622 or equivalent. Reputable suppliers also provide independent third-party test results, positive material identification, and traceability back to the heat number. Never accept pipe without full documentation.
Common outer diameters range from about 1/2 inch up to 8 inches, with wall thicknesses from Schedule 10S to Schedule 80S and sometimes heavier. Custom sizes can be extruded to order, but lead times extend. Always confirm tolerances against ASTM B622 or the relevant standard for your application.
Extrusion forces a heated billet through a die under high pressure, producing a refined, dense grain structure with no longitudinal weld seam. This improves high-temperature strength and corrosion resistance consistency. For HC-22, which is often used in severe service, extrusion helps avoid the weak zones that can occur around welds.
Yes, HC-22 retains good mechanical strength and oxidation resistance at elevated temperatures up to about 1250 degrees Fahrenheit depending on the environment. However, for continuous high-temperature service, you should check the specific temperature limits and consider whether alloy C-276 or another nickel alloy might be more suitable if reducing conditions are present.
Look for a supplier who carries inventory in the sizes you need, can provide cut-to-length services, and has experience exporting to your region. Check their quality certifications like ISO 9001, and ask about their testing capabilities such as hydrostatic testing, eddy current, ultrasonic, or positive material identification. A good supplier also offers technical support for alloy selection and can advise on welding procedures.
HC-22 is often considered an upgrade to C-276 in terms of localized corrosion resistance, especially in oxidizing and reducing mixed acid environments. Compared to Inconel 625, HC-22 generally offers better resistance to pitting and crevice corrosion, though 625 may be chosen for high-temperature strength above 1000 degrees Fahrenheit. The final choice depends on the exact chemical stream and temperature.
Conclusion
HC-22 earns its premium over standard nickel alloys because it holds up in conditions that quickly degrade C-276 or 625—mixed acid streams, hot chlorides, and severe oxidizing-reducing cycles. The balanced chromium and molybdenum content resists pitting and crevice corrosion far longer than older grades, which matters when a leak means lost production, not just a patch job. Extruded seamless construction compounds that advantage by eliminating the longitudinal weld seam, the most common initiation point for stress corrosion cracking in high-pressure systems. The uniform grain structure from extrusion also gives you predictable mechanical properties along the entire pipe length, something welded-and-drawn products struggle to guarantee.
When you're shortlisting suppliers, skip those who only quote price. Ask whether their mill test reports show full heat-lot chemistry, tensile and yield values, elongation, and hardness for every delivery—not just a generic certificate. Inconsistent MTRs, like a missing heat number or an unusually narrow test range, often point to re-rolled or surplus material. Then dig into lead times: custom HC-22 pipe can take sixteen to twenty weeks unless the supplier keeps hollows in stock and runs in-house pilgering. Hidden costs—secondary annealing, straightening, hydrotesting, NDT—should be itemized before you commit. A supplier who voluntarily explains those variables and their impact on delivery is usually the one you can trust for critical service.
Contact Us
Contact Person: Chenji Li
Email: 521 Zhonghui Road, Huishan Economic Development Zone
Tel/WhatsApp: +86 83112233
Website: https://www.jldnickelalloy.com/