Plank Grating Factory: How to Evaluate Quality and Customization Options
2026-08-14
Choosing the right plank grating factory can feel like a gamble—one wrong call and you're stuck with warped panels, inconsistent spacing, or a supplier that vanishes after the invoice clears. Whether you're spec'ing for a chemical plant, a drainage cover retrofit, or an offshore walkway, the real question isn't 'who makes grating?' but 'who makes it right?' At Sino Grating, quality and customization aren't just checkboxes; they're the difference between a floor that lasts a decade and one that fails inspection in a year. In this post, we'll break down exactly how to evaluate a plank grating factory—material traceability, load testing, surface finish—and what customization options actually matter.
Load Ratings and Span Tables: Getting the Numbers Straight Before You Order
Before you place an order for joists, beams, or rafters, pull the manufacturer's span table for the exact product you're buying. Load ratings aren't interchangeable between suppliers—a kiln-dried 2x10 from one mill can carry a different total load than engineered lumber from another. Check the grade, species, and moisture content listed at the top of the table, not just the nominal size.
When you're reading the table, separate the live load and dead load columns. Most residential floors are designed for a 40 psf live load, but if you're planning tile, stone countertops, or a heavy island above, you need to add that dead load to the calculation before selecting a member. Skipping this step is one of the fastest ways to end up with a bouncy floor or an undersized beam.
A common mistake is using a roof span table for floor joists or ignoring the deflection limit notes. If your run has varying spans, size the member for the shortest unsupported distance that will actually carry the load—not an average. And before you finalize the order, have the supplier confirm the table revision on the paperwork matches what's being loaded onto the truck.
Material Grades That Hold Up Under Foot Traffic and Weather
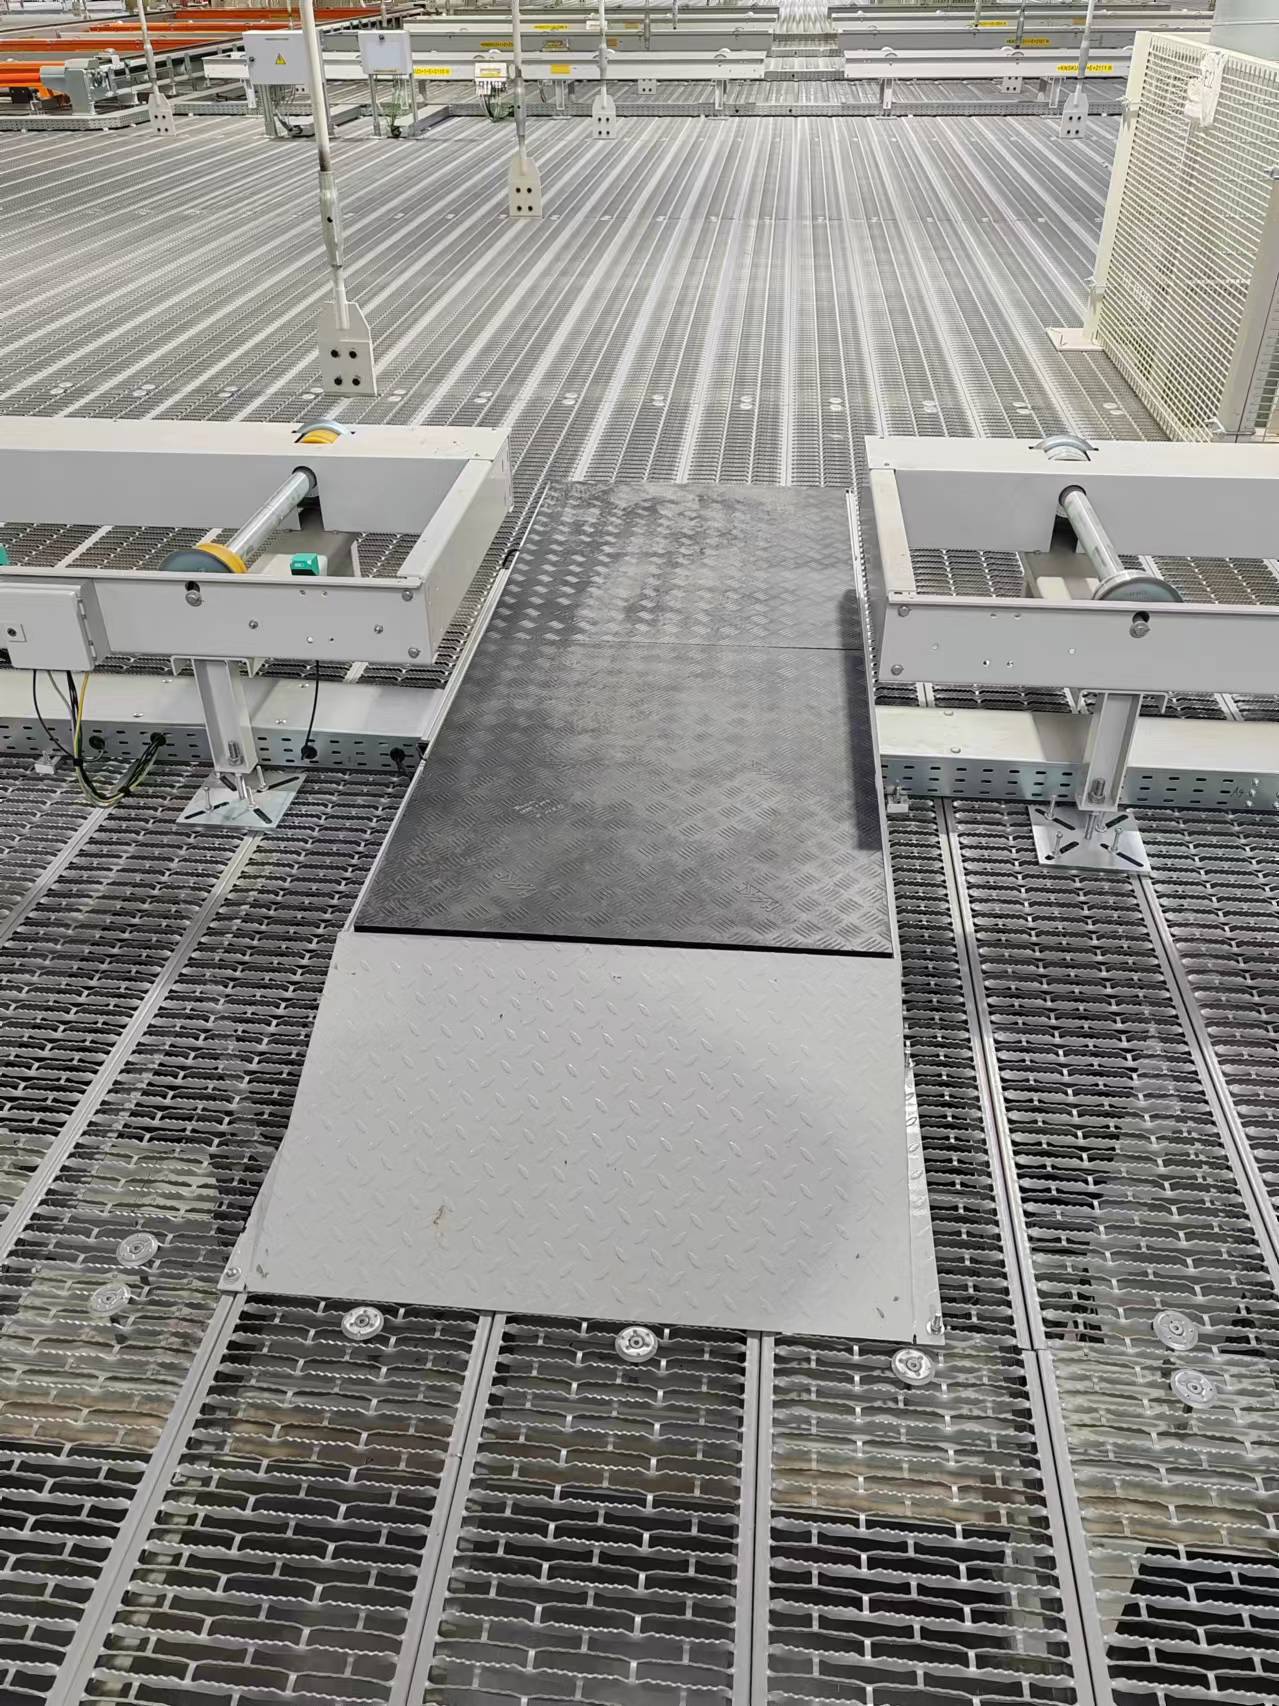
When a walkway or patio gets constant use, the material choice really shows its true colors. You don't want something that looks great on day one but starts showing wear after a single season. For foot traffic and weather combined, look beyond the basic options. Dense natural stones like granite or bluestone hold up well because their tight grain structure resists scratching and moisture penetration. They don't flake or spall easily, even after repeated freeze-thaw cycles. Concrete pavers with a high PSI rating can also work, but only if they're properly sealed and set on a stable base—otherwise, they'll shift and crack under the pressure of boots, carts, or occasional vehicle tires.
Porcelain tile designed for exterior use is another sleeper pick. It's fired at extremely high temperatures, making it nearly impervious to water absorption and staining. The surface doesn't wear down from gritty shoes the way softer limestone or sandstone does. Plus, it won't fade in harsh sun or develop that chalky white efflorescence you often see on cheaper concrete. The key is to check the tile's slip resistance rating—look for an R11 or higher for wet areas—and use a flexible mortar and grout made for outdoor temperature swings. A lot of people overlook this and end up with cracked grout lines after the first hard winter.
If you're dealing with heavy foot traffic plus frequent rain or snow, avoid anything with a polished finish. Polished granite or marble gets dangerously slick when wet, and the shine dulls quickly from abrasive dirt. Instead, opt for a flamed, honed, or bush-hammered texture. Those finishes create microscopic ridges that improve grip and help hide minor scratches. For wood decking, skip the soft pine and go for thermally modified ash or ipe. These dense hardwoods naturally resist rot and don't splinter underfoot, even after years of wet-dry cycling. Whatever you choose, make sure the material grade—not just the type—is specified for high-traffic exterior use. There's a huge difference between a commercial-grade paver and the thin, brittle stuff sold for decorative garden borders.
Custom Fabrication Details That Most Buyers Overlook Until It’s Too Late
Most buyers spend their time checking the big dimensions on a drawing, but it's the tolerance stack that quietly causes trouble later. A bracket might line up perfectly in a CAD model, yet once you add the thickness of powder coat, the variance from a laser cut edge, and the slight offset of a mating part, the holes no longer align. Before you approve a custom fabrication, ask for a tolerance stack-up on any assembly with more than two mating features—it's cheaper to catch that mismatch on paper than after everything has been bent and coated.
Material specifications get glossed over more often than you'd think. Saying "aluminum" or "stainless steel" isn't enough when a sheet metal part is formed along the wrong grain direction and splits, or when a machined edge is left razor-sharp because no edge break was called out. Be explicit about alloy, temper, grain orientation for critical bends, and even the minimum edge radius you expect. The shop may not flag these omissions, and you'll only notice the fatigue crack or chafed wire harness after months in the field.
Welding and finishing details are another place where assumptions get expensive. A fab shop will often choose the fastest weld sequence, which can pull a large flat panel out of flat by several millimeters. Then the beautiful brushed finish you ordered reveals scratches or mill scale because the surface prep wasn't defined. Specify weld locations, sequence constraints, post-weld dressing, and whether you need test coupons for structural joints. It feels like micromanaging, but it's the difference between a part that looks right and one that actually works right.
How to Tell If the Welding and Spacing Are Consistent Across the Panel
Start by looking at the weld beads themselves. Run your eyes along each joint and compare the size, shape, and color of the welds. A consistent weld should have a uniform width and a steady ripple pattern from one end to the other. If you see spots that are wider, narrower, or have uneven penetration, that's a red flag. Also check for undercut, porosity, or cracks—these imperfections often signal inconsistent heat or travel speed during welding.
Next, measure the spacing between welds and the panel edges. Use a tape measure or a caliper to check the gap at multiple points along the seam. The distance should be the same within a tight tolerance—usually a millimeter or less for most panels. Pay attention to corners and curved sections, as these are common places where spacing drifts. A quick way to spot trouble is to hold a straightedge against the panel and see if any welds sit higher or lower than the rest.
Finally, flip the panel over and inspect the back side of the welds. Inconsistent heat can cause burn-through or discoloration on the opposite surface, even if the front looks fine. If you're dealing with a large panel, mark every few inches with a pencil and check those points systematically. Taking a few extra minutes to verify uniformity now can save you from structural failures or expensive rework later.
Surface Treatments and Galvanizing Thickness: What Actually Prevents Rust
When steel is exposed to moisture and oxygen, rust is inevitable unless something interrupts that reaction. Surface treatments like painting, powder coating, or oiling create a physical barrier, but they only work as long as the coating remains intact. A single scratch can let water reach the bare metal, and from there corrosion spreads quietly under the surrounding film. Galvanizing takes a different approach: instead of just sealing the surface, it bonds a layer of zinc to the steel. That zinc doesn't simply sit there passively; it corrodes first, sacrificing itself to protect the underlying metal even at exposed edges or minor damage.
The thickness of the galvanized coating matters far more than most people realize. A thin zinc layer might look shiny and uniform, but it offers limited reserve capacity. Once the zinc is consumed, the steel underneath is on its own. In aggressive environments, such as coastal areas with salt spray or industrial zones with sulfur compounds, a heavier coating can mean the difference between a structure lasting twenty years versus fifty. Standards like ASTM A123 specify minimum thicknesses based on steel type, but on real-world projects, specifiers often push beyond those minimums because the cost of extra zinc is trivial compared to the cost of premature replacement.
Ultimately, rust prevention is not about choosing one method over another; it's about understanding how they fail. A duplex system that combines galvanizing with a topcoat can outperform either alone, because the zinc protects any breach in the paint while the paint slows the zinc's consumption. But if the galvanized layer is too thin, the system collapses quickly once the paint is compromised. So the question isn't whether the surface has been treated, but whether the zinc thickness is sufficient for the specific exposure, and whether anyone checked it with a coating thickness gauge before signing off.
Questions Worth Asking a Factory Before You Sign Off on the Quote
Before you approve that factory quote, pin down how they actually calculate lead times—do they count from deposit receipt, raw material arrival, or production start? A factory that can’t give you a clear, date-stamped production schedule is likely guessing, and guesses turn into “the container was delayed” emails two weeks after your ship window closes.
Ask for a breakdown of material costs and any secondary processes like plating, coating, or printing. If the quote lumps everything into one line item, you won't spot where corners get cut later. Also push for their tolerance policy: what happens when parts arrive slightly out of spec? A solid factory will have a written rework or replacement protocol, not just an apologetic sales rep.
Finally, test their communication rhythm before you sign. How fast do they respond to a technical question? Who owns your project after the order is placed? If you get bounced between three different contacts during the quoting stage, that pattern will repeat during production. Ask for references from a client with a similar product size, and actually call them—five minutes on the phone can reveal more than a stack of audit reports.
FAQ
Start with thickness consistency and bar spacing. If you can get a sample, look for exposed fibers, air pockets, and uneven resin coverage. Reputable shops keep tolerances tight and document them clearly.
Ask which resin system they use—polyester, vinyl ester, or phenolic—and whether it includes UV stabilizers. Request batch certificates for glass content and resin type. A factory that hesitates to share that data often has something to hide.
Beyond panel length and width, they should adjust mesh opening, bearing bar depth, top surface finish, color, and edge trim. Many also handle cutouts, handrail cutouts, and fire-retardant formulations. The best ones will confirm tooling adjustments without long delays.
Look for span tables or third-party test data rather than just a sales claim. The factory should ask about your point loads, distributed loads, and support spacing, then recommend a bar depth and panel size that meets those numbers with a safety factor.
A gritted top surface is the usual choice because it gives solid traction even when wet. Some facilities also offer a concave or meniscus profile, but if slip resistance is the priority, ask for embedded quartz or a coarse grit option and check wear resistance.
Standard panel sizes usually ship quickly. Custom widths, special colors, or non-standard resin systems can add a few weeks, especially if new tooling is involved. Ask the factory to map out the longest-lead component so there are no surprises.
Watch for broad thickness variation from panel to panel, uneven grit distribution, color drift, or bars that look bowed. If there’s no clear batch numbering or traceability, it’s harder to catch a bad run before it reaches your site.
Conclusion
A reliable plank grating factory should give you more than a price per square foot. Pull the load and deflection tables early, and compare them to your actual service conditions—forklifts, pallet jacks, or constant foot traffic all behave differently on a given span. Material selection is just as critical: plain carbon steel may work indoors, but coastal or washdown areas usually demand 316 stainless or a well-specified aluminum alloy. Many buyers also overlook custom details such as radius corners, toe plates, and anchoring holes until the panels are already in production. Looking at sample panels or photos of past jobs can help you judge whether the factory handles these precisely.
Welding consistency and bar spacing often reveal the factory's true quality level. Run your eye along a full panel: welds should be uniform, without burn-through or skipped joints, and the cross bars should sit square to the bearing bars. Surface protection gets even less attention. Ask what galvanizing standard they follow, the minimum coating thickness in microns, and how they verify it after the bath. Also check whether they offer alternatives like paint, powder coat, or duplex systems for aggressive environments. Before you sign off, ask for tolerance limits, inspection records, and a couple of customer references. Factories that answer these questions clearly tend to deliver fewer surprises on site.
Contact Us
Contact Person: Nicholas Zhu
Email: [email protected]
Tel/WhatsApp: 18921275456
Website: https://www.sino-grate.com