Switchgear Tulip Contact Supplier Checklist for Long-Term Reliability
2026-09-14
When a single tulip contact fails, entire switchgear assemblies can go dark. Before you sign off on a supplier, you need a checklist that separates bulletproof contacts from time bombs. MOLDVOLT has spent years refining that vetting process—here's what long-term reliability actually demands.
Certificates That Say One Thing, Load Tests That Say Another
A certificate on the wall says the structure was designed to withstand a certain load, but the actual load test tells a completely different story. The discrepancy rarely comes from a single mistake—it's usually a mix of optimistic assumptions, outdated calculations, and material substitutions that nobody documented. When the test reveals cracks or deflections that the certificate never mentioned, you start to wonder how many other certificates are just nicely framed guesses.
The real problem is that certificates capture a moment in time, while a load test captures the structure as it actually behaves under stress. Concrete that cured differently than expected, steel that came from a different mill, or a contractor who quietly changed the bolt spacing—all of these hide behind a piece of paper that says everything is fine. It's only when you apply the load and watch the numbers climb that the truth comes out, often in ways that make the certificate look like fiction.
This gap between documentation and reality isn't just an engineering annoyance; it's a safety issue that gets papered over until something fails. We need fewer certificates that reassure and more tests that verify, because a load test doesn't care what the paperwork says—it only reports what the structure actually does.
Contact Pressure Checks You Can Do Before Signing Off
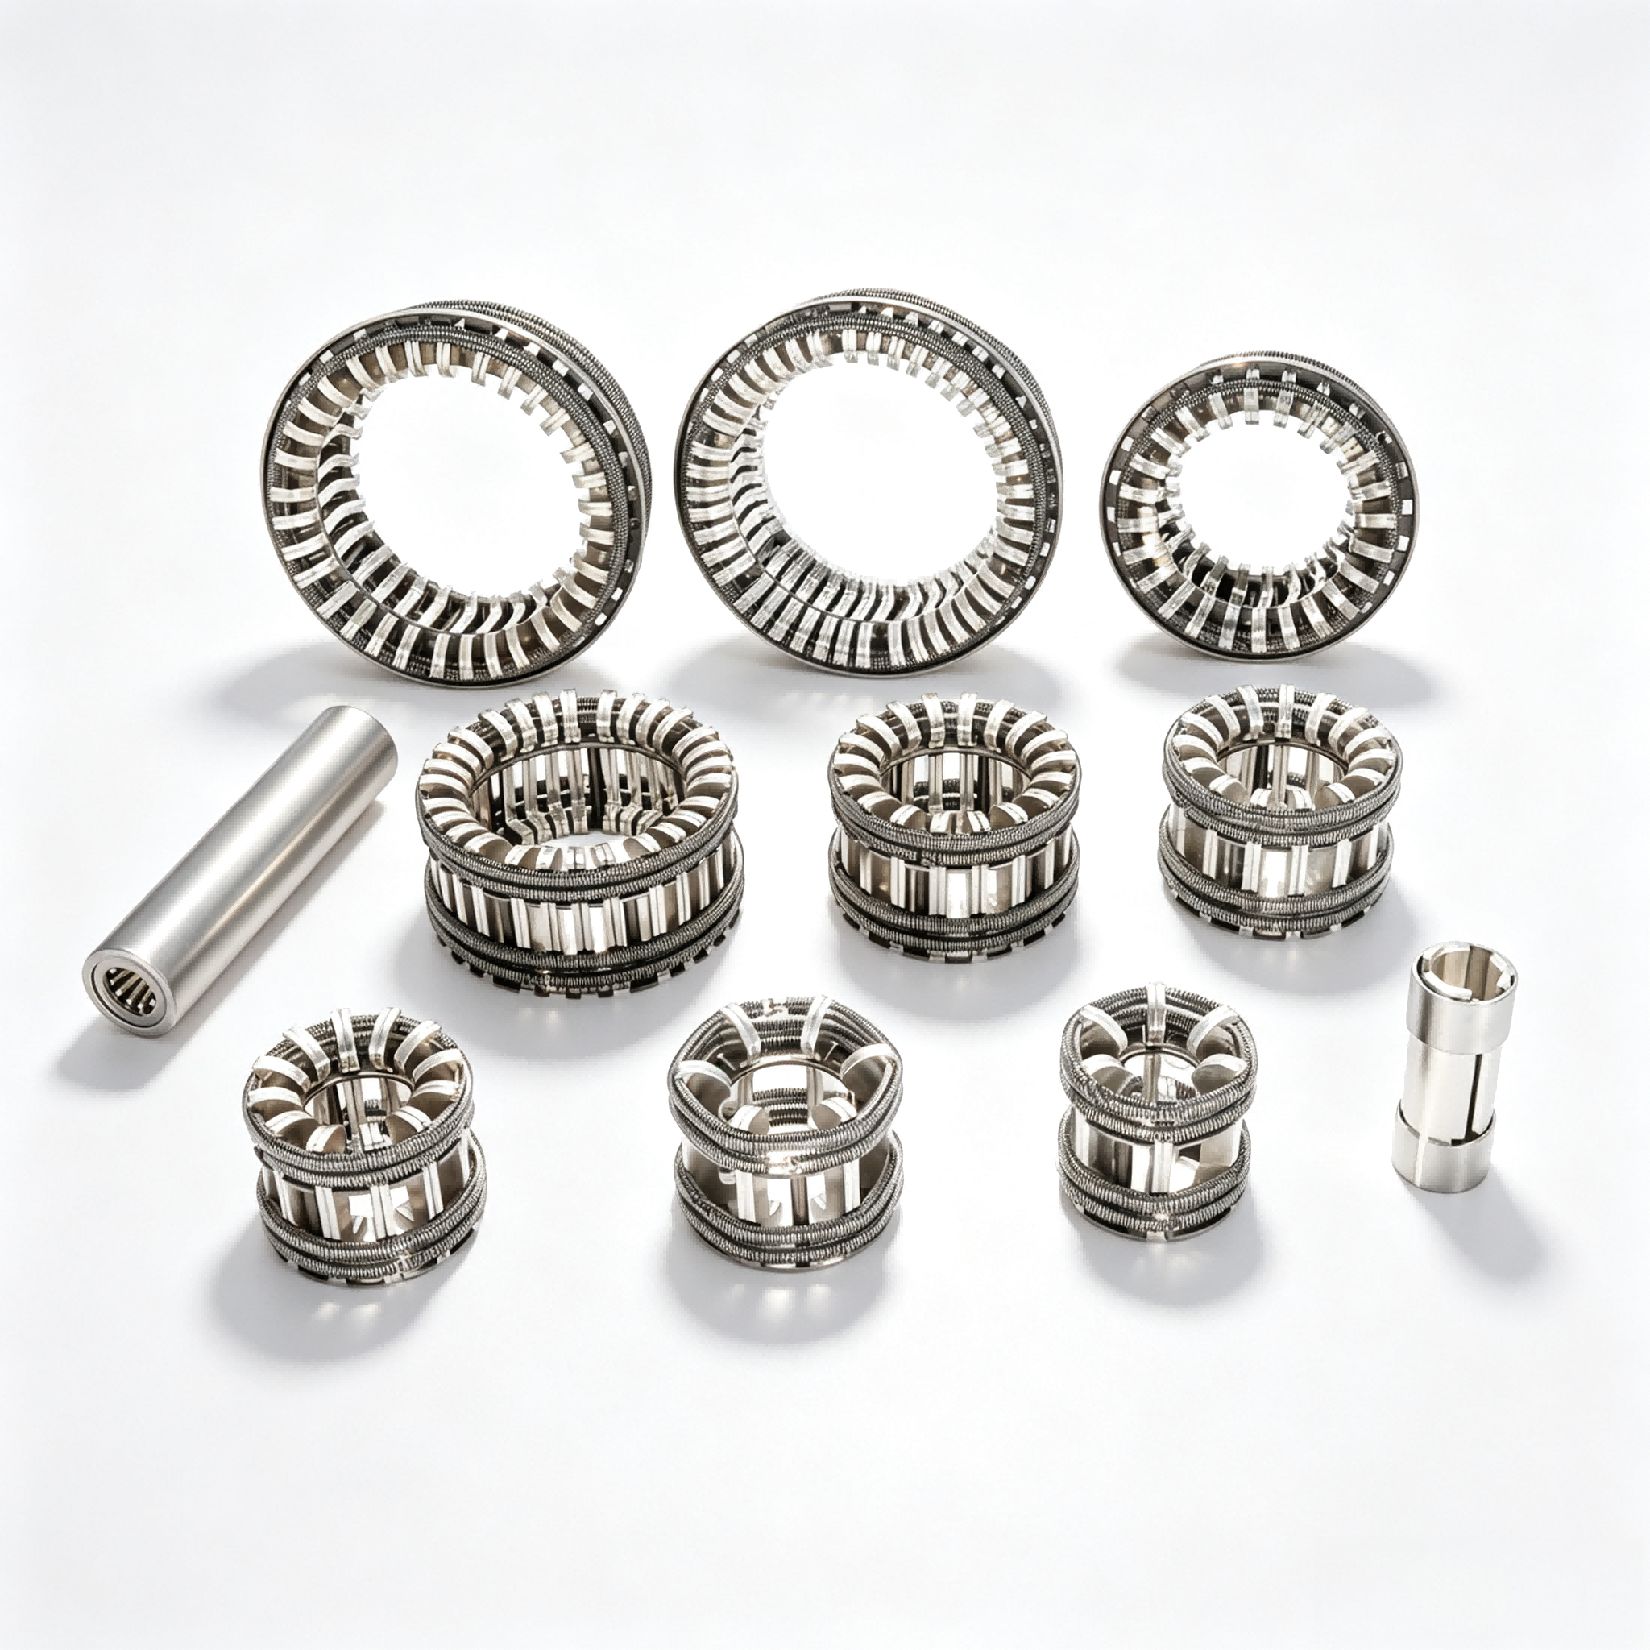
Before you finalize any contact-related design, run through a few hands-on checks that reveal whether the surfaces are truly ready for real-world loading. Start by verifying the actual contact patch under moderate load—use a thin layer of marking compound or pressure-sensitive film, then press the parts together as they would sit in service. Look for uneven distribution, edge loading, or gaps that indicate misalignment. A quick visual scan of the transferred pattern often catches problems that simulation missed, especially around fillets, chamfers, or slightly warped mating faces.
Next, pay attention to how the contact area responds when you introduce a small amount of cyclic motion or vibration by hand. You can rock the assembly gently, apply a light torque, or tap near the interface while watching for relative movement. If you feel any play, hear a clicking sound, or see fretting dust forming after just a few cycles, the preload or surface finish is likely insufficient. This kind of manual probing mimics early-stage service conditions and exposes weak spots before they become full failures.
Finally, remember to check the contact force decay after assembly. Tighten the fasteners or apply the clamping load, wait a few minutes, then re-measure the gap or preload. Many materials relax slightly under initial compression, especially polymers, composites, or rough machined surfaces. A simple feeler gauge or torque wrench recheck can show whether the contact is settling into a stable state or slowly losing grip. If the numbers shift more than expected, reconsider the surface roughness, material pairing, or bolt pattern before you sign off on the design.
Tooling Logs Expose More Than Any Audit Checklist
Most audit checklists document what a team intends to do, or what a policy says should happen. Tooling logs, on the other hand, capture what actually got executed—every command, every failed retry, every manual override. That gap between intention and execution is where real risks hide, and a static checklist rarely has the resolution to see it.
Consider the small deviations that never make it into a formal review. A developer temporarily disables a security scan to meet a deadline, or an operator tweaks a resource limit without updating the runbook. These moments show up in tooling logs as anomalies, but they’re invisible to any checklist that focuses on approved configurations and documented procedures.
Moreover, logs provide sequence and context. A checklist can confirm that a step was marked complete, but it cannot show that the step ran out of order, took three times longer than expected, or produced a warning that was ignored. Tooling logs expose the texture of real work—hesitations, workarounds, and shortcuts—giving you a much sharper picture of operational reality than a signed-off list ever could.
Silver Plating Adhesion: The Test Many Suppliers Skip
Walk into most plating shops and you'll see racks of freshly silvered parts gleaming under fluorescent lights. What you won't see is anyone pulling a strip of tape off those parts to check if the silver actually stays put. Adhesion testing is the unglamorous step that gets skipped when deadlines loom and orders pile up. Yet it's the difference between a connector that survives five insertion cycles and one that flakes out in the field within a week. Many suppliers treat adhesion as an afterthought because visual inspection can't catch a weak bond—the plating looks perfect until mechanical stress or thermal cycling reveals the truth.
The most common adhesion tests are straightforward: a tape pull, a bend test, or a thermal shock cycle. None require expensive equipment, and all can be done in minutes. So why do so many suppliers skip them? Often it's because they rely on a generic process recipe rather than validating it for each substrate and batch. Silver plating over copper, brass, or steel each demands different pre-treatment—activation, striking, or underplating—and cutting corners there shows up as poor adhesion later. A supplier that doesn't test is essentially betting that their process never drifts, which is a risky wager with temperature, chemistry, and bath contamination all in play.
When plating adhesion fails, the symptoms are rarely subtle: silver flakes peel away from contact surfaces, leading to increased resistance, intermittent connections, and premature wear. In high-vibration environments or tight-fit assemblies, even microscopic delamination can escalate into costly field returns. The irony is that the fix is cheap compared to the fallout—a simple tape test or a cross-hatch evaluation before parts leave the line would catch most issues. Suppliers who skip this step aren't saving time; they're just transferring the failure downstream to their customers.
Batch Drift Is the Silent Reliability Killer
When a model first ships, its test results look solid. But production data rarely stays still. Batch drift creeps in as user behavior changes, upstream systems get patched, or seasonal patterns shift. The dangerous part is that no single batch triggers an alert—each one looks acceptable on its own, yet cumulatively the model slides further from the reality it was trained on.
Engineers often catch the problem late because dashboards track aggregate accuracy over weeks or months. By then, the model may have been confidently serving wrong predictions for a while. Drift doesn't announce itself with a crash; it weakens outputs quietly, turning a reliable system into a source of subtle, compounding errors.
Treating batch drift as a first-class operational concern means checking input distributions per batch and comparing them to the training baseline. Without that discipline, you're not maintaining a model—you're just waiting for a silent failure to surface.
Thermal Cycling Data Points That Actually Matter
Most thermal cycling reports bury the lead in total cycle counts. What actually predicts field failures is the delta between peak and minimum temperature at the solder joint, not just chamber air temperature. A 40°C swing with a fast ramp can do more damage than an 80°C swing soaked for hours, because strain rate changes how cracks initiate in intermetallic layers. Track ramp slopes, dwell at each extreme, and the first signs of resistance drift—an early jump of 5% often signals a crack long before open circuit.
Dwell time matters less than getting the board to thermal equilibrium. If you ramp the chamber but the PCB is still lagging by 15°C, you are not testing the part you think you are. Add board-level thermocouples at the hottest component and the coldest spot in the enclosure, and record the lag time. Then set cycle count based on failure distribution, not a pass/fail fixture: when three consecutive cycles show no further resistance change, the crack has stopped growing and further cycling is just waiting for a new failure mode.
FAQ
Focus on the contact finger geometry, especially the radius at the throat and the wiping angle. Ask for CMM reports showing consistency across batches, not just a single golden sample. Verify that the finger thickness matches the rated current and that the tulip’s inner diameter tolerance stays within the spring compression range under all specified operating temperatures.
Request cross-sectional micrographs of the plated fingers, not just thickness readings. The plating should have a uniform thickness across the curved contact zone, with no exposed copper at edges. Ask for hardness values and adhesion test results per ASTM B571 or equivalent, and specify a minimum plating thickness at the wear points rather than an average over the whole finger.
Look for constant-force or multi-turn compression springs made from corrosion-resistant alloys. Check the spring’s stress relaxation data at the maximum rated temperature over 10,000 hours. The spring should maintain at least 85% of its initial force after thermal aging. Avoid designs where the spring directly carries current, as this can cause annealing and loss of clamping pressure.
Ask for a control plan that includes incoming raw material certificates, batch traceability for copper and silver, and in-process inspection records for crimping or brazing of the contact fingers to the conductive body. A meaningful supplier will share field failure data or teardown reports from installations older than 10 years, not just laboratory test certificates.
Insist on a four-wire measurement with a defined test current and a specified mating bar diameter. The acceptance limit should be stated in micro-ohms at a reference temperature, and the supplier should test after thermal cycling, not only on virgin parts. Ask whether the fixture applies the same insertion depth and alignment as the actual circuit breaker.
High-conductivity tellurium copper or chromium-copper alloys offer better resistance to softening than pure ETP copper. Check that the supplier specifies the alloy temper and provides hardness readings after forming and brazing. If fingers are stamped, ask about grain direction and residual stress because these affect stress relaxation and cracking after years of thermal cycles.
Conduct a continuous current test at rated current with the contact assembled in the actual breaker or a thermally equivalent fixture. Monitor temperature rise at the finger-to-bar interface and the spring. The contact should stabilize below the standard limit, and the supplier should provide data showing no progressive increase in contact resistance during the test. Add a cyclic overload test to simulate emergency conditions.
Watch for vague statements like “high-quality silver plating” without thickness or adhesion specs, springs sourced from unknown sub-suppliers, no mention of thermal aging or stress relaxation, and an unwillingness to share dimensional capability studies. Another red flag is using pure ETP copper without any temper specification for high-current fingers.
Conclusion
Certificates from a tulip contact supplier can look flawless while the contacts themselves fail under real load. Before you sign off on any batch, run your own contact pressure checks with a calibrated force gauge rather than trusting factory data; a simple insertion and removal sequence won't catch weak clamping force until it is too late. Tooling logs are far more revealing than any standard audit checklist because they capture worn dies, skipped maintenance, and undocumented parameter tweaks that no certificate will mention. When those logs show irregular wear or frequent adjustments, treat it as an early warning even if the current samples pass.
Silver plating adhesion is the test many suppliers skip, yet it decides whether the plating flakes off after repeated mating cycles. Batch drift quietly compounds this risk: minor shifts in copper alloy temper or plating thickness from one lot to the next can push contact resistance upward over time. Pay close attention to the thermal cycling data points that actually matter, such as resistance rise after several hundred hot-cold cycles, spring force retention after heat soak, and contact temperature at rated current. These measurements expose the slow degradation that certificates and one-off load tests hide, and they are the only solid basis for accepting a supplier long term. If you ignore these, you inherit failures that only show up years later in the field.
Contact Us
Contact Person: Hellen
Email: [email protected]
Tel/WhatsApp: 86-13634205622
Website: https://www.voltcabinet.com